- Visual assessments remain vital but are influenced by lighting, fatigue, and sample handling.
- Standardized testing conditions improve consistency but cannot eliminate all variability.
- Better training and comprehensive quality strategies align lab results with actual product performance.
Color fastness is still considered one of the most crucial aspects of textile quality control because it directly influences how a fabric looks and performs, especially after rubbing, washing, exposure to light and regular day-to-day wear. For mills, labs and retailers alike, this is not just a small detail; it is central to product quality, keeping customers happy and maintaining a good brand image. Industry groups like RISE and testing companies such as Eurofins and Intertek have noted that if colors don’t stay put, it can lead to complaints, cut down on how long a product lasts, and erode trust in the finished product.
That’s why testing for color fastness has become such a key part of evaluating textiles. The tricky part is not just figuring out if a sample changes color, it is also whether the methods used can really capture that change in a way that is consistent and useful. The article from TESTEX stresses that labs can do plenty to reduce variation, things like proficiency checks, comparisons with other labs,and tightly controlling the testing environment. But, at the end of the day, it is clear that technical procedures alone don’t totally remove all uncertainty.
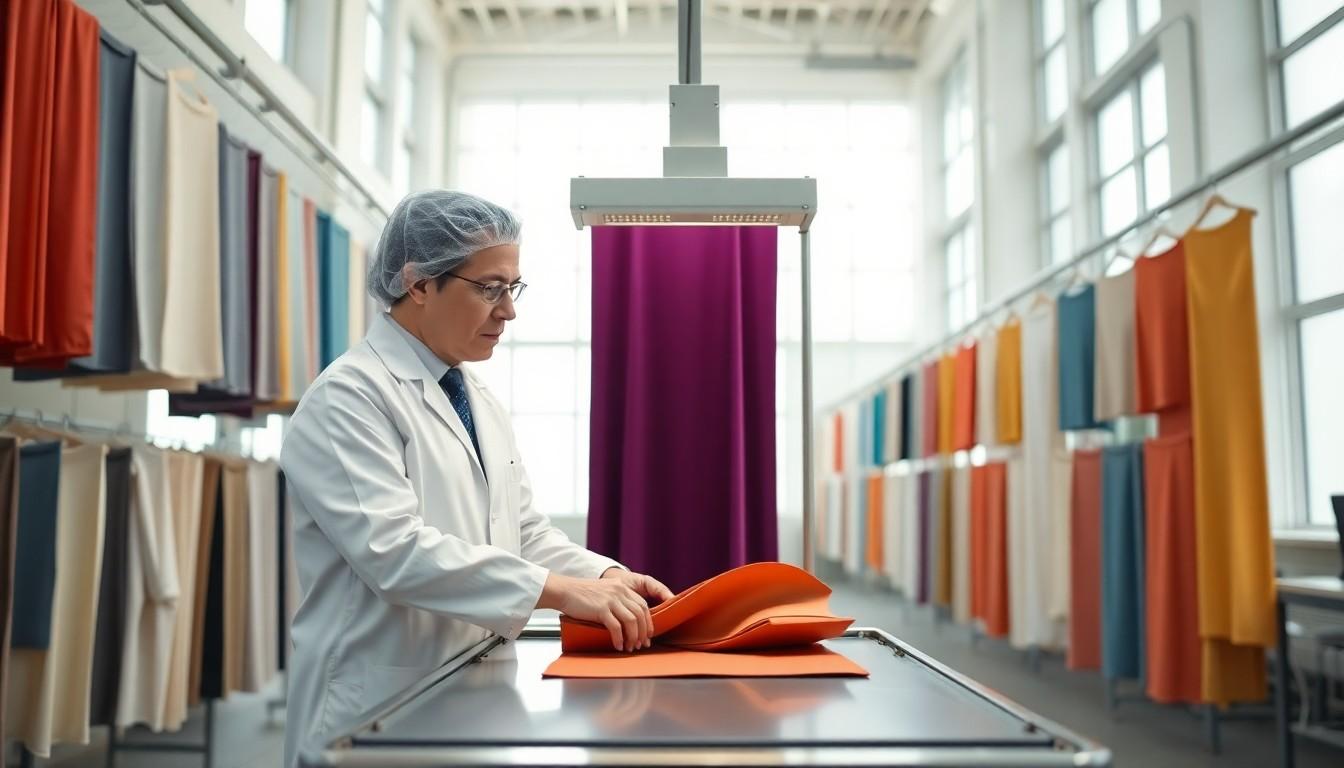
A big challenge here is that a lot of the evaluation still relies heavily on trained inspectors comparing tested samples against reference standards, then grading them based on what they see. But the outcome can be influenced by a variety of factors that are often overlooked. The lighting conditions can make a sample look quite different. Fatigue might mess with an inspector’s focus. Even how the fabric is prepared and presented can introduce distractions. Plus, the order in which fabrics are reviewed can subtly change how an observer perceives the colors.
Sample handling, for instance, is one of those steps people often forget, yet it can shape the results even before the actual comparison begins. The article points out that both the original and tested pieces should be cut neatly and aligned in the same fabric grain. Also, they need to be prepared so that seams, background paper and other distractions don’t skew the final reading. Special care is especially needed for printed fabrics, jacquards, pile materials, loosely woven fabrics and heavily finished cottons, all of which can have textures, gloss, shrinkage or pile directions that change how the color appears.
Lighting matters just as much as how samples are handled. The article says visual assessments should use standardized light sources, like D65, with neutral gray surroundings, to limit reflections and any bias in the colors. It also mentions that evaluation methods can vary depending on whether a textile is matte, slightly shiny or highly glossy, and that inspectors might need to look at fabrics from different angles, because surface reflection can skew the way we see the color. When doing rubbing tests, inspectors need to judge both the color change and any staining, then compare these results against the appropriate gray scales used in textile testing.
All this points to a larger idea: color fastness testing is not just about passing or failing, but really about understanding how textiles will behave in real life. It gives manufacturers insight into whether a garment might fade after washing, or if dye transfer might cause issues for customers or nearby products. The TESTEX article wraps up by suggesting that better training, disciplined observation and stable working conditions can really improve the reliability of tests. Meanwhile, the industry as a whole continues to push for standardized methods to make sure results are more consistent across different labs and supply chains.
For sourcing teams, this matters long before bulk production begins. A fabric that looks acceptable in a showroom or on a mobile screen can still fail in actual use if its dye chemistry, finishing process or fiber blend is not well controlled. That is why early sourcing decisions should consider not only color shade and hand feel, but also the expected performance of the textile under washing, rubbing, perspiration and light exposure.
In logistics, color fastness also connects to how products travel and store over time. Garments may sit in warehouses, move through humid shipping lanes, or be packed tightly with other goods before reaching the customer. Even if a textile passes lab testing, poor handling in the supply chain can create quality issues that look like manufacturing defects. This is why quality control has to extend beyond the lab and into packaging, warehousing, and distribution practices.
For brands tied to lifestyle products, color stability is part of the customer experience. Consumers expect a shirt, curtain, towel, or home textile to keep its appearance after repeated use. When colors fade too quickly or stain adjacent materials, the product may feel cheap or unreliable, even if its construction is otherwise sound. In a market where visual appeal strongly shapes purchasing decisions, maintaining color integrity supports both repeat business and long-term brand trust.
The same is true for retailers working with seasonal collections or fast-moving inventories. A mismatch between lab results and real-world wear can create returns, complaints, and markdown pressure. Reliable fastness evaluation helps reduce those risks, making it easier to plan assortments, manage claims and keep product quality aligned with customer expectations.
Takeaways
- - Color fastness is a core textile quality metric, not a minor detail.
- - Visual assessment still matters, but it is vulnerable to lighting, fatigue and sample preparation issues.
- - Standardized conditions help, yet they do not eliminate every source of variation.
- - Better training and controlled environments improve confidence in results.
- - Sourcing and logistics teams should treat fastness as part of the full product lifecycle, not just a lab result.
- - For consumers, good color fastness usually means better durability, better appearance and fewer disappointments.
FAQ
Why is color fastness so important in textiles? Because it affects how long a fabric keeps its appearance and whether it performs well after washing, rubbing and light exposure.
Can visual testing be fully replaced by instruments? Not always. Visual judgment is still widely used, but it must be supported by standardized methods and consistent conditions.
What makes some fabrics harder to evaluate? Printed fabrics, jacquards, pile materials, loose weaves and heavily finished textiles can all distort how color appears.
What should brands and sourcing teams focus on? They should look at both appearance and durability, and make sure testing reflects real-world use as closely as possible.
Disclaimer: This article may have been created with AI assistance and reviewed by our editorial team. It is provided for general informational purposes only. Readers should verify information independently before relying on this content.
Sources: