- Clarify revision control and product class for accurate inspection
- Combine visual, microsection, and electrical testing for comprehensive evaluation
- Ensure documented evidence and proper anomaly management to maintain quality
How to Effectively Apply IPC-A-600 in Bare PCB Inspection
IPC-A-600 still stands as the main visual guide within the industry for assessing bare printed circuit boards, but its usefulness depends on how you use it, not just treating it as a standalone verdict. According to IPC and other industry explanations, the standard helps inspectors classify what they see on unassembled boards and judge those observations against specific acceptance criteria. Those criteria cover both internal and external features.
This distinction is important for electronics manufacturers, sourcing teams, contract manufacturers, and quality specialists alike. IPC-A-600 offers a structured way to evaluate a board’s condition, but it does not replace the performance requirements or other specifications that a particular product needs to meet. A strong inspection process uses the standard as one part of a controlled quality system.
For companies involved in global sourcing or electronics logistics, this approach helps create a common language between the buyer, fabricator, receiving team, and engineering department. Without a shared understanding, the same lot of boards can be viewed differently at various points in the supply chain.
Revision Control is Key First
The most recent version of the document is IPC-A-600M, which IPC says was released in May 2025. Buyers and suppliers should not automatically assume that a newer revision overrides the one tied to an existing purchase order, drawing note, or approved quality plan.
In practice, the applicable revision is the one specified by the controlled requirements for the project or program. An order might refer to a specific version of the standard, and an engineering drawing or quality agreement may include additional instructions. Review these documents together rather than interpreting them separately.
A good rule is to record the exact revision in controlled manufacturing records. This helps fabrication, receiving, engineering, and supplier quality teams assess the same lot against one consistent baseline. If an older product moves to a new revision, review the changed requirements, affected features, and inspection instructions together.
Explicit Class Selection Matters
Choosing the right class, whether Class 1, 2, or 3, is often oversimplified. IPC and other guides describe these as different service levels: Class 2 is for dedicated-service electronics, while Class 3 covers higher-performance applications where continued operation is especially important.
The customer, drawing, or contract should clearly define the applicable class. Do not assume it based only on the end market or product category. An industry label or general notion about reliability is not enough; the requirement must be documented.
For sourcing teams, the class should be explicit before the job is released. This is particularly important for programs spanning automotive, industrial, medical, or communications hardware. The acceptance class should be established by the customer or the responsible engineering team.
The goal is not necessarily to choose the most demanding class by default. The class should match the product’s actual requirements, with the decision made intentionally before production begins.
Use IPC-A-600 Alongside Companion Requirements
This standard should be read together with the applicable requirements for rigid and flexible boards. IPC indicates that IPC-A-600 aligns with companion standards, while industry guidance emphasizes distinguishing bare-board acceptability from assembly acceptability.
IPC-A-600 concerns the condition of the unassembled PCB. Assembly acceptability standards address the completed electronic product. These standards are not interchangeable.
A board might look good visually and still fail because of electrical or structural issues. Conversely, a well-soldered assembly might contain a bare-board issue. Keeping the stages separate improves traceability and helps identify whether a problem originated in the board, the assembly process, or an interaction between them.
Always Inspect Features, Requirements, and Evidence
When inspecting, it helps to ask three questions: What am I looking at? What criterion applies? What supports my decision?
The inspector identifies the feature or condition being checked, such as the board outline, holes, conductive traces, solder mask, exposed lands, or overall surface condition. Next, the applicable requirement is identified. Finally, the evidence supporting the decision is recorded.
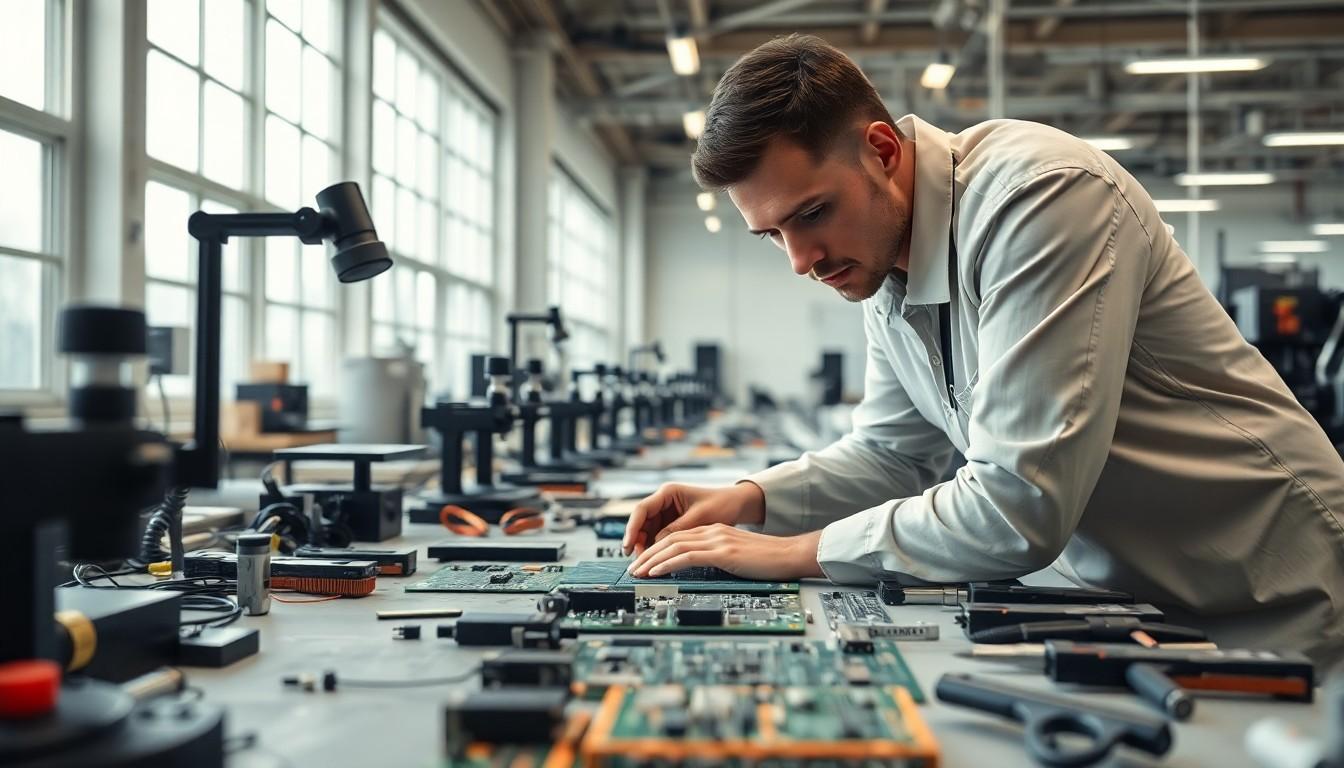
Use suitable lighting, magnification, and measurement tools for the feature being examined. These tools support consistent evaluation and comparison with documented criteria; they do not make every board condition a failure.
A clean surface does not guarantee electrical integrity, and a visible flaw does not automatically require rejection. Each decision should be tied to the relevant requirement. Inspection records should state what was examined, how it was examined, and why the conclusion was reached. Include measurements or photographs when needed, rather than recording only “pass” or “fail.”
Recognize When Visual Inspection Isn’t Enough
Surface views alone may not adequately reveal an internal feature. Microsection analysis is appropriate when the required assessment concerns internal construction that surface inspection cannot show or when the inspection plan specifies it.
Cross-sections can help evaluate features such as hole wall quality, copper structure, laminate integrity, resin fill, and internal interconnections. A microsection does not replace routine inspection; it answers questions that surface inspection cannot address.
The verification plan should match the board’s actual structure. This is particularly important for high-density interconnect (HDI) builds, where microvia interfaces, filled or capped vias where specified, and interconnected via structures may require feature-specific examination. A simple through-hole view is not a substitute for evaluating a complex microvia chain.
Before selecting a sample, define what the section must demonstrate. Record the panel or lot, coupon identity, feature location, preparation method, and measurement results. Preparation artifacts must be distinguished from conditions present in the original board.
Inspect According to the PCB Construction
The inspection plan should follow the construction being manufactured. Common board checks can be applied consistently, but additional examinations may be needed for features that a simpler construction does not contain.
For FR-4 printed circuit boards, inspect drilled features, surface lands, and the interconnections actually present in the stack-up. Relevant build information includes layer definition, finished holes, copper, and surface finish.
For HDI construction, pay particular attention to microvia interfaces, fill or cap requirements where specified, and interconnected via structures. The via map, sequential build description, and relevant coupon requirements should be available to support the evaluation.
For rigid-flex circuits, inspect coverlay openings, bonded areas, and transitions between flexible and rigid regions. The rigid/flex boundary, coverlay and stiffener drawings, and intended bend conditions should be understood before inspection.
A universal form can miss these differences. Use a common record structure, but make the feature list and evidence requirements specific to the part being released.
Electrical Testing Offers a Different Kind of Evidence
Electrical testing measures something visual inspection cannot: connectivity and isolation under controlled conditions. A board might look fine under magnification but still require electrical verification to confirm that intended connections are present and unintended connections do not exist.
Link test results to the released design data, netlist, program revision, test conditions, and board or lot identity. After a design revision, verify that the test data changed with it. Reusing an old program can produce a reassuring result for the wrong connectivity.
Reports should be precise rather than using vague “IPC passed” summaries. Visual acceptability, electrical integrity, impedance, solderability, cleanliness, and other specified evaluations require their own methods and acceptance conditions.
Manage Anomalies Through Containment and Disposition
When an inspection identifies an anomaly, contain the affected material and establish the applicable requirement before deciding disposition. Do not accept a questionable lot merely because assembly is waiting, or reject it solely because its appearance differs from an ideal illustration.
Identify the affected board, panel, and lot, and keep suspect material separate. Record the feature, location, measurement, and examination conditions. Check the document revision, class, drawing notes, and approved exceptions. Determine whether additional measurement, sampling, or testing is needed, then obtain an authorized disposition and retain it with the supporting evidence.
If documents conflict, resolve the issue through the controlled engineering process. An informal statement that a board “looks acceptable” should not become an undocumented relaxation of a production requirement. Recurring issues should be tracked through trend and corrective-action records.
Certification and Documents Do Not Prove Lot Conformity
An IPC-A-600 certification credential concerns personnel knowledge within a training and assessment program. It does not, by itself, prove that a particular delivered lot meets its requirements. Keep personnel credentials separate from manufacturing records, inspection results, and the product conformity statement.
Likewise, an IPC-A-600 PDF found online may be an older edition or an incomplete excerpt. Use an authorized copy of the applicable revision for acceptance decisions. A web article, training summary, or illustration cannot replace the complete criteria and agreed specification for the board.
Key Takeaways
- - Confirm the required IPC-A-600 revision before inspection.
- - Document the applicable product class rather than assuming it.
- - Use IPC-A-600 alongside construction, performance, and assembly requirements.
- - Match inspection methods to the PCB’s actual construction.
- - Support decisions with measurements, photographs, test results, and traceable records.
- - Use containment and authorized disposition procedures for anomalies.
- - Treat certification documents as supporting information, not proof of lot conformity.
Disclaimer: This article may have been created with AI assistance and reviewed by our editorial team. It is provided for general informational purposes only. Readers should verify information independently before relying on this content.